Mark Hedley Jones
OmioCNC EPL Post-Processor
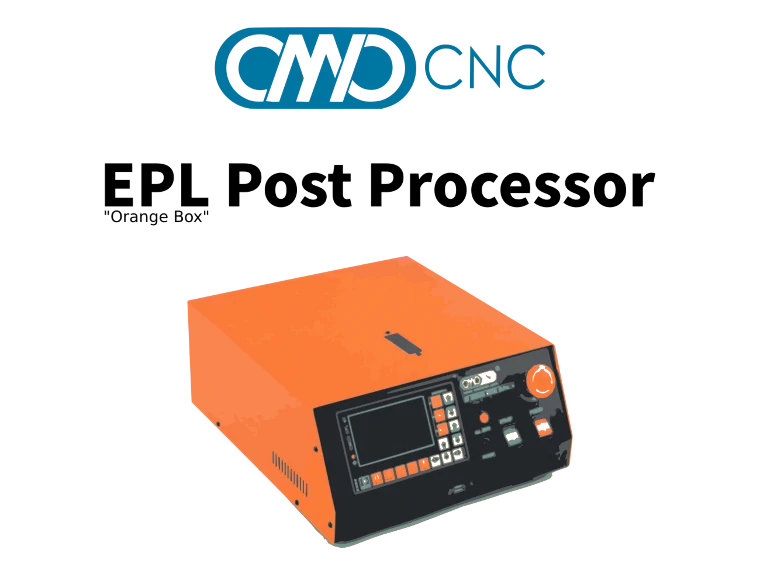
After purchasing a X8-2200EPL from OmioCNC, I found incompatibilities between its "orange box" controller and the machining commands produced by Autodesk software such as HSM Express, HSMWorks and Fusion 360. The built-in GRBL postprocessor could be used with the machine but the controller misinterpreted the commands for curves/arcs.
By creating various test cases I determined the issues lay with how the controller was interpreting the compact .nc files that the GRBL postprocessor was generating. I noticed that the default GRBL postprocessor omits X, Y, and Z coordinates between commands if those coordinates don't change between commands. The orange box doesn't like this. Instead of assuming those coordinates remain the same and continuing on, it would use different values (I didn't spend the time to figure out where those values came from). I wrote a custom post-processor - the step that translates toolpaths into machine commands - to include those coordinates explicitly and match the controller's numerical precision. Using this custom post-processor the OmioCNC Orange Box runs smoothly.